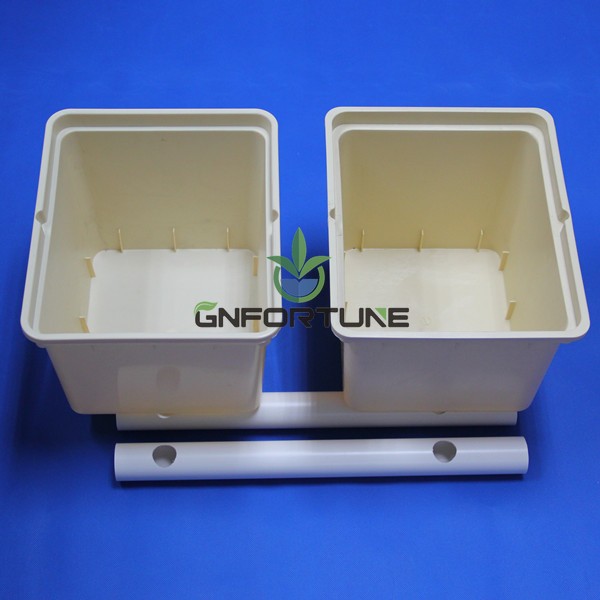
A Dutch bucket spends its life holding several litres of solution, a heavy vine, and its own shape, outdoors. A net pot holds a wet substrate plug at a precise height for the whole crop. Both fail quietly when moulded badly — and because injection moulded hydroponic buckets look identical on a product page, the manufacturing details are worth knowing before you compare prices.
This guide explains the process, the resin decisions that matter, the defects that predict field failures, and what a buyer can check without visiting the factory.
What Is Injection Moulding and When Is It Used in Hydroponics?
Injection moulding melts plastic pellets and injects them under high pressure into a steel mould, where the part cools in seconds and is ejected. It is the right process for discrete, thick-walled, three-dimensional parts — Dutch buckets, net pots, tray components, lids and fittings — where extrusion cannot form the geometry.
The economics follow from the mould. A mould costs real money and takes weeks to cut, but once it exists, every additional part is cheap. That is why standard bucket and net pot designs are priced far below custom variants, and why OEM colour or logo changes are usually simple while geometry changes are not.
Which Resin Should a Hydroponic Bucket Be Made From?
| Resin | Strengths | Trade-offs |
|---|---|---|
| HDPE | Tough, good impact resistance, flexible at low temperature, excellent chemical resistance | Slightly less rigid; can creep under long static load if wall is thin |
| Polypropylene (PP) | Stiffer, higher temperature tolerance, good fatigue resistance for living hinges | More brittle in cold conditions without impact modifiers |
| Recycled blend | Lower cost | Uncontrolled contamination and stabiliser levels — unsuitable for nutrient contact parts |
For nutrient-contact parts, virgin resin with a UV stabiliser package is the specification that matters, and it should appear on the datasheet. A bucket formulated for years outdoors and a commodity bucket differ mostly in what you cannot see.
What Defects in Moulded Parts Predict Field Failures?
- Short shot: incomplete filling, seen as thin or missing sections at the rim or rim lip — the part will split there under load.
- Weld lines: visible flow-join marks where two melt fronts met, typically near the drainage sump — a built-in crack path on a stress point.
- Warpage: the bucket rocks on a flat table — it will never sit level on the row, and level matters for drainage height.
- Sink marks and flash: local thin walls or unmoulded edges along the rim, where clips and lids seat.
Any one of these on a sample is a process-control signal, not just a cosmetic flaw. Moulded-part quality is statistical: a good line produces thousands of identical parts, so a defective sample implies a defective batch.
How Does Cycle Control Affect the Parts You Receive?
Injection quality lives in the boring parameters: melt temperature, injection pressure and speed, holding pressure, cooling time. Rush the cooling phase and parts leave the mould hot and shrink afterwards — arriving warped even though they looked fine at the machine. Run holding pressure low and sink marks appear over thick sections like the bucket base.
This is why moulding capacity is a real signal when choosing a supplier. A factory that owns its moulding workshop controls its own cycle parameters and can hold dimensional consistency across an order of tens of thousands of units. A factory that subcontracts moulding learns about your problem when you do.
How Can a Buyer Check Moulded Quality Without a Factory Visit?
- Request a datasheet naming the resin and stabiliser package for nutrient-contact parts.
- Order samples and stress them: seat and remove the lid ten times, press the base, stand the bucket on glass to check rock, fill with water to check level and drainage.
- Compare several samples from different cartons — consistency across cartons is the real test.
- Ask which parts are moulded in-house and which are bought in, and where the moulds are held.
Ten minutes with samples and a flat table tells you more than an hour of product-page reading.
FAQs About Injection Moulded Hydroponic Buckets
What plastic are Dutch buckets usually made from?
Commercial Dutch buckets are most commonly HDPE or polypropylene, both of which resist the nutrient salts and pH range used in hydroponics. The specification that matters is virgin resin with UV stabilisation for outdoor service, declared on the datasheet. Recycled blends should be refused for nutrient-contact parts regardless of price.
Why do cheap net pots crack after a season?
Usually a resin problem or an aggressive cycle: insufficient UV stabiliser, recycled content, or parts ejected too hot that have shrunk into internal stress. The rim and the slot roots are the crack initiation points. Fresh samples from a current production batch, stressed by hand, expose most of these before you order.
Can I get my own logo or colour on moulded parts?
Colour is straightforward — masterbatch changes within an existing mould. Logo embossing requires a mould modification, which is practical and common in OEM arrangements. A full geometry change means a new mould, with cost and lead time to match, so it is worth deciding before the first order rather than after.
What MOQ applies to moulded products?
Moulded parts are quoted per piece rather than per metre, and minimums are typically set by the economics of a production run and the packing carton. Standard stocked designs carry lower minimums than custom variants. Confirm MOQ, colour and packaging together, because all three move together in the quotation.
Is in-house moulding really better than subcontracting?
For consistency and response, yes. An in-house workshop controls cycle parameters and can adjust or re-run quickly; a subcontractor adds a layer between your defect report and the machine that made the part. In-house capability also protects your lead time during peak season, when subcontractors allocate capacity to their largest accounts first.
What to Send When You Request a Quotation
For a moulded-product quotation, send: part and variant (bucket size, net pot rim and height), quantity, colour and any branding requirement, destination port and target order date. With those five items a factory can quote the real number including packaging, instead of a range that moves later.
Related reading: decide the system first in Dutch bucket vs NFT, run vine crops with the Dutch bucket tomato guide, buy net pots in volume with the wholesale net pot buying guide, and structure branding via OEM and private-label manufacturing.
Send the part, quantity and colour you need, and we will quote including moulding, packaging and lead time: contact our team.