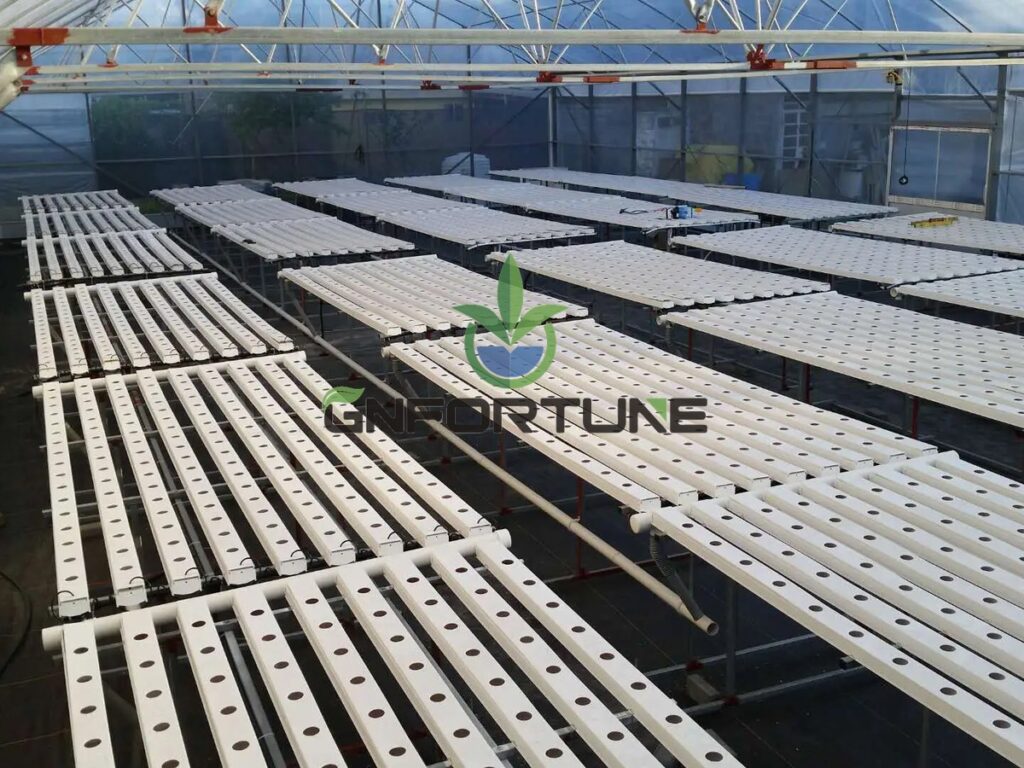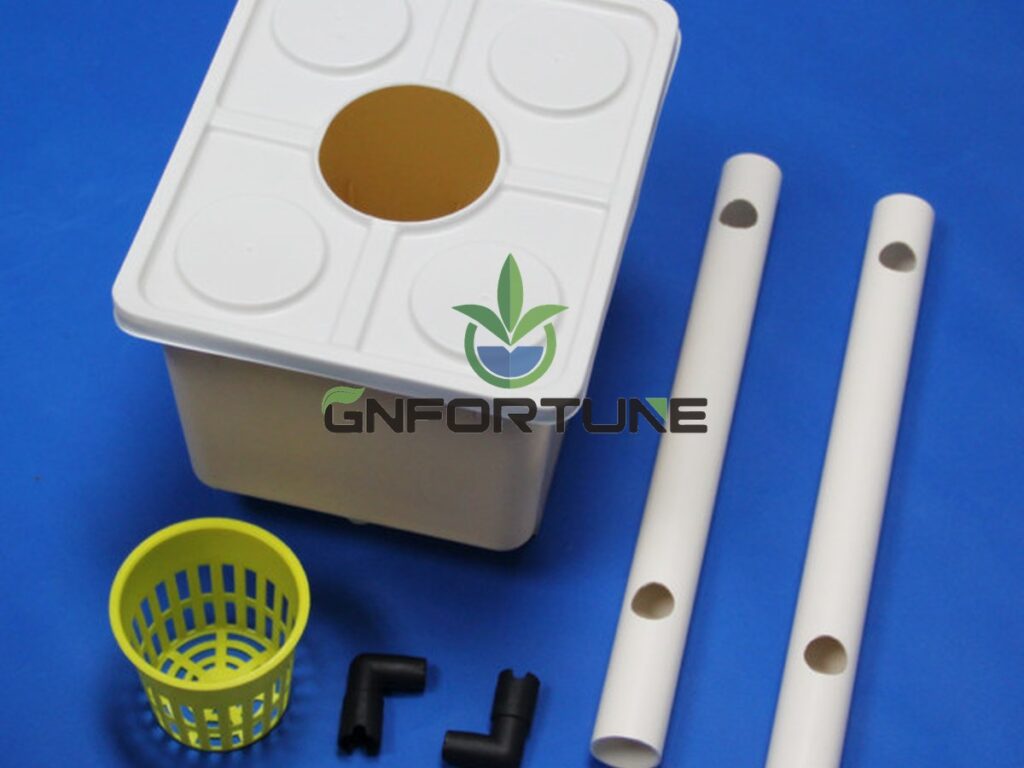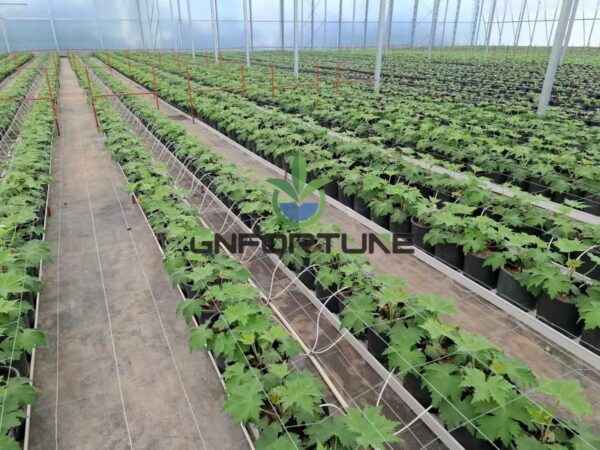
The question is rarely “which is cheaper” — it is “which route carries the specific risk this order has”. A hydroponic equipment distributor buys, holds and resells; a manufacturer owns the extrusion line, the tooling and the production schedule. Those are different products even when the carton holds the same channel. This comparison is for buyers selecting a route per order rather than per relationship, because most commercial projects use both at different stages.
What Each Route Sells You: Manufacturer vs Hydroponic Equipment Distributor
A manufacturer sells production capacity and control over specification. A hydroponic equipment distributor sells availability, small quantities and a local counterparty. Neither is automatically the better equipment sourcing route, and the difference shows up in what each can change on your behalf.
| Manufacturer (factory direct) | Distributor / stocking partner | |
|---|---|---|
| What you are buying | Extrusion or moulding capacity, tooling, material specification | Inventory already landed, mixed SKUs, someone local to call |
| Specification control | High — profile, wall thickness, material grade, colour, length, OEM marking | Low — limited to what has been imported |
| Typical quantity | Container-scale, tied to a minimum production run | Carton or pallet, up to whatever stock is held |
| Response speed | Slower on first order, predictable on repeats | Fast when in stock, slow when they must reorder |
| Technical depth | Design-level: drawings, tolerances, system sizing | Practical: installation familiarity, faster swap-outs |
| Best fit | Projects, custom profiles, repeat expansions | Spares, top-ups, mixed small orders, urgent replacement |
Two other intermediates appear in hydroponic supplier selection and should not be confused with either. An agent represents the factory for a commission, and the factory still ships and invoices. A trading company consolidates across several factories — useful for mixed orders, less useful when a specification needs defending.
Cost Structure Behind the Same Product
The same channel leaves the same factory in both routes. The difference is which layers sit on top, and the only comparison that means anything is landed cost per metre or per unit at your site.
- Ex-works factory price. The base both routes start from, though a distributor with volume may negotiate a lower base than a single project buyer.
- Distributor margin. Trading margin plus inventory carrying, inland freight, customs clearance and local delivery.
- Freight and duty. Paid in your name when factory direct, or embedded in the distributor’s landed cost — embedded is not the same as absent.
- Credit cost. Local-currency terms with 30–60 days are often worth real money to a farm with a working capital gap, and that value belongs in the comparison.
- After-sales provision. A distributor’s price includes someone who answers a claim locally; a factory price may not, so make the difference explicit.
Factory direct tends to win on container-scale volume, custom specification and repeat orders; distributors win on small mixed orders, urgent replacement, and where their consolidated container beats an LCL rate. The break-even sits near container utilisation and SKU count, so price both for the actual order rather than in principle.
Whichever route is chosen, quotes have to be normalised before they are comparable — the method in comparing hydroponic equipment quotations applies equally to a factory and a distributor response, and the request behind both should follow how to write an RFQ that gets comparable quotes.
MOQ, Consolidation and Freight
Hydroponic equipment MOQ at a factory is usually a production constraint rather than a commercial policy: a minimum run length before an extrusion line is stable, a minimum batch before an injection moulding change is economic, and a minimum quantity per colour. Minimum order quantities therefore differ by profile, colour and length, and they are worth asking about per SKU rather than per order.
- Per-profile and per-colour minima. A colour change adds changeover waste, so a second colour in the same order can carry its own minimum.
- Length and packing. Standard packing lengths are what fill a container efficiently; odd lengths raise freight per metre.
- Volumetric reality. Channels and gutters are long and hollow, so freight is often governed by volume rather than weight. Nesting, bundling and container utilisation matter more than the rate itself.
- Consolidation. A distributor’s real advantage is mixing several factories’ products into one container. Where an order is diverse and individually below factory minima, that consolidation can beat factory direct on total landed cost even with margin on top.
Consumables are the usual consolidation candidate: media, fittings and small parts shipped with the main equipment order cost far less per unit than a separate top-up — see growing media wholesale: pallets, MOQ and freight and NFT channels wholesale bulk buying.
Lead Time and Production Slot Reality
Factory direct means waiting for a production slot; going through a hydroponic equipment distributor means waiting for stock, and if there is no stock it means waiting for their reorder cycle on top of the factory’s. “In stock” is the distributor’s only genuine time advantage, so the first question is whether the quantity is actually on their floor.
Factory lead time is a production slot plus the run, packing and export booking. Changes after the run starts are expensive or impossible, and peak-season slots tighten, so booking early beats expediting later. Custom tooling adds time once, and every repeat order is then faster.
Distributors reorder on their own cycle: a profile they do not hold means waiting for their next consolidation, which can be longer than ordering direct. Confirming stock by photograph and count rather than by spreadsheet avoids that surprise.
Technical Support, Drawings and After-Sales
Factories are stronger on specification and drawings; distributors are stronger on language, time zone and physical presence. The distributor’s technical depth depends entirely on who they employ, so test it rather than assume it.
Questions that separate a technically capable counterparty from a reseller:
- Can they issue a dimensional drawing with tolerances for the exact profile being quoted?
- Can they confirm material grade and UV stabilisation in writing, and whether the same grade applies across repeat orders?
- Can they state flow rate and slope assumptions for the channel or gutter, and size the return main accordingly?
- Who signs off spare parts availability three years after commissioning?
- Who attends if irrigation uniformity or installation sequence is disputed on site?
For long-cycle and phased projects, any support promised by a distributor should be backed by the manufacturer in writing. A distributor can change principals; the tooling and the profile cannot easily change with them. Spares planning belongs in the same conversation, and dispatch practice is described in factory direct dispatch of bulk hydroponic orders.
Risk: Warranty, Claims, Currency
The risk difference between the routes is about who absorbs a problem, not about which route has fewer problems. Write the answer into the contract before the order rather than discovering it during a claim.
- Warranty. Who honours it, in which country, and whether it covers only the part or also labour and return freight. A factory warranty often requires packing and loading evidence and leaves freight to the buyer; a distributor handles it locally but may lack authority to approve a replacement without referring back.
- Claims. Shortage, dimensional and damage claims all depend on evidence captured before the container is sealed. The checks that generate that evidence are covered in factory QC before an order ships.
- Currency and payment. Factories commonly price in USD or EUR against T/T terms; distributors may invoice in local currency with credit. Compare the credit’s value against the price difference rather than treating it as a free extra.
- Continuity. Ask whether the profile, tooling and material grade will still be available for the next phase; expansion orders that cannot match the first batch create two spares inventories.
- Concentration. Single-sourcing is efficient until the counterparty changes. A named second source for consumables is cheap insurance.
Score the counterparty after delivery, not at purchase. A simple record of dimensional accuracy, packing condition, document accuracy and claim response makes the next route decision evidence-based — see supplier scorecards for rating vendors after delivery.
Choosing by Project Stage
Most projects should split the route rather than pick one. The table is a starting allocation; adjust it where local stock, credit terms or a custom specification change the balance.
| Project stage | Recommended route | Why |
|---|---|---|
| Sampling and validation | Factory direct sample set, or distributor if speed dominates | Specification questions are answered by the manufacturer; a distributor helps only if the same item is already imported |
| First project build | Factory direct for the system, local for ancillaries | Drawings, tolerances and container-scale volume matter most at this stage |
| Expansion phase | Factory direct, repeating the same specification | Matching the earlier batch protects spares, labour training and irrigation uniformity |
| Consumables and media | Consolidate with the main order, or distributor for top-ups | Freight per unit dominates; small urgent top-ups favour local stock |
| Spares holding | Distributor for fast movers, factory for critical spares | Balances response time against supply certainty for parts that stop production |
| Emergency replacement | Distributor | Downtime cost exceeds the price premium for anything already on the shelf |
FAQs About Hydroponic Equipment Sourcing Routes
Is factory direct always cheaper?
No. Factory direct wins on container-scale volume, custom specification and repeat orders, but a distributor consolidating several factories into one container can beat a direct LCL shipment on landed cost even with margin. Compare landed cost per unit for the actual order.
Why is the factory MOQ higher than the distributor’s?
Because it is usually a production constraint rather than a sales policy: minimum run length on an extrusion line, batch size for a moulding change, minimum quantity per colour.
Can a distributor provide drawings and material certificates?
Sometimes, but the manufacturer is the source. Ask for a dimensional drawing with tolerances and written confirmation of material grade and UV stabilisation; if the distributor cannot obtain those, the route is unsuitable for a project specification.
Who handles warranty claims under each route?
The party you contracted with. A distributor can process a claim locally but may need manufacturer approval; a manufacturer will usually require packing and loading evidence and may leave freight to the buyer.
Should a project use one route throughout?
Rarely. Factory direct for the system and expansion phases, distributor or consolidated ordering for consumables, spares and urgent replacement is the allocation that works on most sites.
Related Reading
- Comparing Hydroponic Equipment Quotations: How to Normalise Bids — How to normalise bids so the two routes are actually comparable
- Hydroponic Equipment Lead Times: Full Path — The full lead time path from order placement to dispatch
- How Hydroponic Equipment Ships: Container Loading, MOQ Math — Container loading, MOQ maths and what freight does to unit price
- Hydroponic Supplier Factory Audit: The Checklist Buyers Use Before Placing an Order — The factory audit checklist buyers use before placing an order
- Factory-Direct NFT Channels: How We Dispatch Bulk Hydroponic Orders — How bulk factory-direct orders are dispatched
Next Step: What to Send for a Quotation
A route can only be priced against a defined order. Quantity per SKU, whether the specification is standard or custom, and whether the shipment is a full container or a consolidation into one decide which route is cheaper — and they are the inputs most often missing from an enquiry.
For a project quotation, send: site or greenhouse dimensions and layout drawing, crop and system type, quantity per SKU or total metres required, whether the profile is standard or custom, packing and length preferences, destination port or delivery address, target delivery date and budget range, and whether the enquiry is factory direct or through a hydroponic equipment distributor. G AND N FORTUNE LIMITED manufactures NFT channels, Dutch buckets, DWC and substrate gutter systems in a 5,000 m² factory with in-house extrusion and injection capacity, and quotes against project parameters.