Grade is decided in the greenhouse and confirmed at the packing bench — never created there. Grading standards for hydroponic produce exist to turn a buyer’s written specification into daily decisions made by graders, and the farms that get paid consistently are the ones where those two things are the same process.
This guide explains how specifications are written, how to build grading into the line, where defects actually originate, and which records resolve a dispute when a load is challenged on arrival.
What Are Produce Grading Standards?
Grading standards are the written criteria that decide whether a unit of produce is saleable, at what grade, and in what pack. They cover size or weight range, count per pack, colour and maturity, freedom from specified defects, and the tolerance — the percentage of units allowed to fall slightly outside specification.
Most retail specifications in this sector follow a two-class structure, with a premium class permitting almost no defect and a second class allowing minor blemishes within defined limits. The tolerance figure matters as much as the defect list: it is what separates a pass from a rejection on a borderline pallet.
How Is a Supermarket Specification Actually Written?
Specifications are written by the buyer’s technical team and usually run to several pages per product. They are unambiguous about the things the buyer can check at the distribution centre — weight, count, pack integrity, temperature on arrival, labelling — and necessarily more subjective about appearance.
Read a specification in this order, and translate it into something a grader can apply in two seconds:
- Defect list: what is unacceptable at all, and what is acceptable within limits.
- Tolerance: the percentage permitted per pack or per load.
- Size or weight band: the range, and how to handle units outside it.
- Pack format and count: carton, bag, punnet, weight or count per unit.
- Conditions of delivery: temperature, pallet configuration, labelling and traceability codes.
Anything ambiguous should be clarified before the season, with a written answer. Ambiguity resolved after a rejection is resolved in the buyer’s favour.
How Do You Build Grading Into the Line?
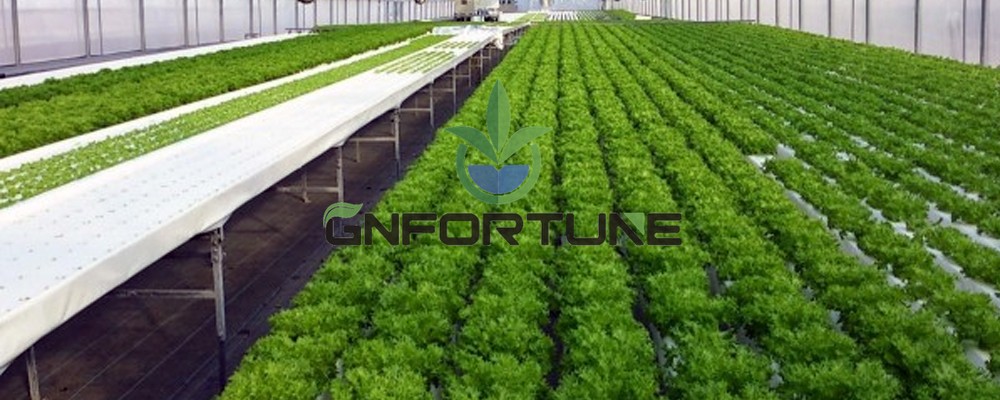
Grading works when the grader has the information, the light and the time to apply the standard. Four elements matter more than equipment:
- Specification at the bench: the buyer’s defect list printed, laminated and visible, with photographs of accepted and rejected units.
- Lighting: neutral, bright and consistent — poor light hides exactly the discolouration and early rot that a spec is written to catch.
- Line speed matched to grader capacity: a conveyor that outruns the graders sets the standard, not the specification.
- Reject categories recorded: every rejection tagged by cause, so the information travels back to growing or handling.
| Common defect | Usual origin | Where to intervene |
|---|---|---|
| Tipburn on leafy crops | Calcium transport under fast growth and low transpiration | Airflow, root-zone EC, growth rate — not the packing bench |
| Bruising and splitting | Handling, over-tight packing, harvest too mature | Harvest timing, crate fill height, packing pressure |
| Discolouration and slimy leaves | Field heat, delay to cooling, wet packing | Time to cooler, drain before packing, cold chain |
| Underweight units | Spacing, short cycle, light deficit | Crop plan and spacing — grading only detects it |
| Foreign matter and contamination | Floor hygiene, crate sanitation, loose debris | Hygiene zoning and crate washing |
Which Records Resolve Disputes?
Disputes are settled with evidence, and the farms that win them have three things on file for every load: grading records showing what was inspected and by whom, photographic examples of the accepted standard at dispatch, and temperature records from cooling through to loading.
Add a retained sample from each dispatch, held under the buyer’s storage conditions for the stated shelf life. When a load is challenged, a retained sample from the same pallet converts an argument into a comparison.
What Mistakes Undermine a Grading Operation?
The first is grading in poor light, which hides the defects being looked for. The second is letting line speed set the standard — inspectors rushed to keep pace with harvest pass borderline product, and borderline product is the reason a load is downgraded on arrival.
The third is failing to record reject categories, which removes the link back to growing and guarantees the same failure repeats. The fourth is leaving second-grade destinations unplanned: if the only outlet for rejects is compost, every quality failure becomes a total loss instead of a price discount. Decide the second-grade channel before the season and re-price it whenever volumes change.
FAQs About Hydroponic Produce Grading
What is the difference between Class I and Class II?
Class I requires produce to be of good quality with only very slight defects within tight tolerance; Class II allows minor defects and slightly wider tolerance while remaining marketable. Buyers specify which class they accept, and mixed-class loads are usually rejected rather than downgraded.
How much tolerance is normally allowed?
Tolerance varies by buyer and product, commonly around 5–10% of units per pack failing minor criteria. It is specified in the buyer’s document rather than by regulation, so confirm the figure for each product and pack format before quoting volumes.
Who should do the grading?
Trained graders who did not grow the crop, working to a printed specification with reference photographs. Growers grading their own output consistently over-grade; rotating graders and refreshing the reference samples keeps the standard stable across the season.
What should happen to second-grade produce?
Plan the outlet before the season — processors, wholesale markets, food service packs or farm shops. Without a planned channel, second-grade volume becomes waste; with one, it recovers a meaningful share of production cost.
How is grading linked to traceability?
Each packed unit should carry a code linking it to house, bed or batch and pack date, recorded at dispatch. When a buyer raises an issue, that code lets you trace back to the growing records and forward to other affected loads in hours rather than days.
What to Send When You Request a Quotation
Crop and weekly volume, pack formats required, buyer specification if available, available floor area and existing cooling capacity. Packing and grading equipment should be sized to the grading standard, not only to harvest throughput.
Related reading: pack formats are covered in packaging formats and shelf life, cooling requirements in post-harvest cold chain, line design in harvest and packing line automation, and traceability in batch records that pass an audit.
Send your crop, weekly volume, pack formats and buyer specification, and we will size grading, packing and cooling to that standard: contact our team.