The Water You Already Paid to Move
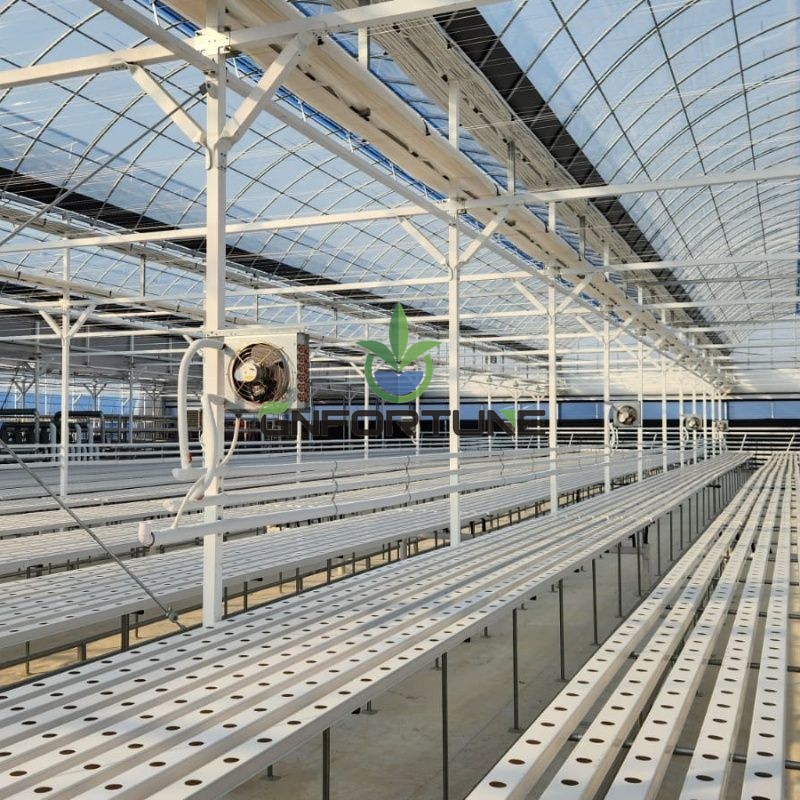
Every chiller, air handler and dehumidifier on a hydroponic farm produces water. A 10,000 m² cooled greenhouse in a humid climate can drip out 20–60 m³ of condensate per day in peak season — clean, cool, almost mineral-free water that most farms send down the drain. On sites where water is metered, permitted or scarce, that is a resource being discarded daily.
Condensate recovery hydroponics is not complicated engineering. It is a small collection circuit, a holding tank, basic treatment and a rule for how the water may be blended back. This guide covers the practical side: where the water comes from, what is in it, and how to put it back to work safely.
Where Recoverable Water Appears
| Source | Typical volume | Quality notes |
|---|---|---|
| AHU and chiller condensate | 0.3–1.2 L per kWh of cooling | Near-distilled; picks up coil dust and biofilm |
| Dehumidifier condensate | 2–8 L/m²/day in peak transpiration | Can carry volatile organics from air |
| Chilled-water loop blowdown | System-dependent | Contains inhibitors — never reuse without testing |
| Roof and gutter rainwater | Climate-dependent | Good volume; needs first-flush diversion |
| Reverse osmosis reject | 20–40% of RO feed | Saline; usable only for flushing or tolerant crops |
Condensate and RO reject are the two most mishandled streams. Condensate is almost always reusable; RO reject almost never is for fertigation, but is excellent for washing floors and irrigation lines.
What Is Actually in Condensate
Condensate is essentially distilled water that has touched dust, coil surfaces and drain pans. The risks are not mineral — it is biological loading from warm, wet surfaces and occasional coil treatment chemicals. The standard precautions:
- Slope and flush drain pans so no standing water ages in the system
- First-stage filtration — 100–150 mesh at the collection point
- UV or slow disinfection if the water feeds propagation or foliar systems
- Sample monthly for bacterial counts while the system is young, quarterly once proven
- Never recover from coils treated with biocides unless the label permits
The one chemistry point that matters: condensate has no alkalinity and almost no calcium. It cannot simply replace source water — it must be blended.
Blending Rules That Keep Recipes Stable
Your nutrient recipe is written against a known source water analysis. Condensate changes the blend, so control the proportion rather than the instinct:
| Use | Max share of condensate | Why |
|---|---|---|
| Stock tank make-up | 100% | Mineral-free water is ideal for concentrates |
| Seedling and propagation misting | 100% after UV | No foliar deposits on young leaves |
| Main fertigation blend | 30–50% | Keeps calcium and trace background stable |
| Drain-to-waste open systems | Up to 70% | Recipe recalculated at the dosing station |
| Equipment and line flushing | 100% | No mineral value needed |
The safest implementation is a two-tank day-store: one tank of source water, one of condensate, with the dosing controller drawing a fixed ratio. Staff cannot then improvise.
Sizing the Collection Side
- Tank size for 1–2 peak days of production, not the annual average
- Overflow to drain — the tank must fail safe, not flood the plant room
- Level monitoring tied to the farm alarm system, so a dry tank never runs a pump
- Material choice — opaque HDPE or covered tanks to prevent algae growth
- Dedicated pump, not a shared wash-down pump that back-contaminates
Retrofit cost on a mid-size farm is usually a few thousand dollars in tankage, pipework and a UV unit. Against metered water plus wastewater charges, payback in water-stressed regions is commonly under two seasons.
What the Numbers Look Like
Work the sum for your own site before investing: (daily condensate m³) × (water + sewer cost per m³) × (operating days). A farm recovering 30 m³/day at $2.50/m³ combined is banking roughly $22,000 a year — before counting the reduction in RO feed demand and the resilience benefit when municipal supply is interrupted.
There is also a commercial angle: buyers and auditors increasingly ask about water-use efficiency per kilogram of produce. A documented recovery circuit is evidence, not just savings.
FAQ
Is condensate safe for hydroponic use?
Yes, once filtered and disinfected. It starts cleaner than most source water; the risks are biological, from drain pans and tanks, and are handled by hygiene and UV.
Can condensate replace RO water entirely?
Often it can, and at a fraction of the energy cost. RO produces roughly 0.3 m³ of permeate per kWh; condensate arrives already separated. Sites running both usually keep RO only as backup.
Does recovered condensate affect the nutrient recipe?
Only through blending. Keep the share of condensate in the main blend fixed and have the recipe calculated for that mixture, then nothing drifts.
What about condensate from packaging rooms or cold stores?
Collect it, but keep food-area condensate separate from plant-room condensate until tested. Any water from food-handling areas is held to hygiene standards, not just irrigation standards.
Is rainwater collection worth adding at the same time?
If roof area is available, yes — the same tank and treatment serve both, and rainwater brings useful calcium and sulphate background that condensate lacks.
Will auditors accept recovered water?
Yes, when you can show the treatment steps, sampling records and blending rules. Documented recovery generally scores better than potable-only supply in water-efficiency audits.
Small Circuit, Compounding Value
Condensate recovery is one of the few farm upgrades that pays in water, energy and audit standing at the same time. If you are specifying a new system, tell us the climate and cooling load and we will size the collection side with the layout. Start with the quote form.
Related reading: this connects to the wider water plan — see reservoir and storage tank design, water treatment options, blending with marginal water, chiller sizing and nutrient temperature and reading your water analysis.