Every Plant Moves Several Times Before It Is Sold
A seedling starts in a propagation room, moves to a nursery bay, is transplanted into a production channel, is inspected and worked in place, is harvested into a crate, is cooled, is packed, and is stored before it leaves. That is five to seven touches per plant, multiplied by every plant on site, and almost none of those touches are decided by the growing system. They are decided by the layout around it.
Hydroponic farm logistics is the least glamorous topic in a project and one of the fastest ways to lose money. This guide covers the route design decisions that should be made on paper before the first gutter is hung.
Start With the Crop Flow, Not the Building
Draw the product route as a single line from propagation to dispatch, then force it to be one-way. Every place the line doubles back on itself is a place where clean and dirty traffic meet, where trolleys pass each other in a narrow aisle, and where a worker walks an extra few hundred metres a day.
- Propagation — seed, germinate, raise plugs
- Establishment — move plugs into the production system, hold in a nursery zone
- Production — crop work, inspection, the long residence time
- Harvest — cut, weigh, crate, remove from the growing area
- Cooling and packing — the first stage that is not a growing environment
- Storage and dispatch — cold store, loading bay
- Waste and empties — the reverse flow nobody plans for and everybody needs
Note item seven. Green waste, empty crates, spent substrate and packaging all move in the opposite direction to the crop, and if they share the same aisle as harvested produce you have both a hygiene problem and a traffic problem.
Aisle Widths and Access: The Numbers That Matter
| Route | What moves on it | Design consideration |
|---|---|---|
| Main spine | Trolleys, pallet trucks, people | Must allow two-way traffic or be formally one-way with passing points |
| Working aisles between rows | One worker, hand tools, harvest crate | Wide enough to work in comfortably for a full shift, not just to squeeze through |
| Headlands at row ends | Turning trolleys, transfer, machinery | Frequently under-designed; this is where turning happens, not the aisle |
| Propagation to production transfer | Trays and trolleys of plugs | Minimise distance and level changes between the two climate zones |
| Harvest to cool room | Loaded crates, time-critical | Shortest practical route; a long hot journey undoes the cooling |
| Waste out | Green waste, empties, spent media | Separate from produce route wherever the building allows |
Two rules of thumb worth arguing about early: nobody should have to reverse a loaded trolley repeatedly during a shift, and no product should ever pass through a dirty zone to reach a clean one.
Transfer Points Are Where Time Disappears
Every transfer — tray to channel, channel to crate, crate to pallet — costs time and creates a damage risk. Count them in your plan and try to remove at least one.
- Standardise container sizes. Trays that fit the trolley, crates that fit the pallet, and pallets that fit the door save more time than any single piece of equipment.
- Match bench and trolley heights. Repeated lifting from ankle height to shoulder height all day is an injury claim waiting to happen, and a productivity tax every day until then.
- Keep a buffer at the transfer point. Enough space for a few minutes of staged work absorbs normal variation instead of blocking the aisle.
- Put a surface under the transfer. Cuttings and drips happen at transfers; a washable floor and a drain in the right place keep it from becoming a hygiene issue.
Mechanisation: What Actually Pays
Automation is not a single decision. On most commercial sites the order of return looks like this: layout first, then handling equipment, then measurement, then automation.
| Investment | Typical benefit | Watch out for |
|---|---|---|
| Aisle and headland design | Immediate labour saving, no capital | Requires committing area to access instead of plants |
| Trolleys, benches, height-matched work surfaces | Large gain in handling time and reduced injury | None significant; usually the best early spend |
| Weight-based harvest recording | Makes yield and labour measurable per bay | Only useful if someone reads the data weekly |
| Conveyors and packing line automation | High throughput, consistent pack | Needs volume to justify; assumes upstream is stable |
| Robotic transplanting or harvesting | Labour substitution at scale | Highly crop and task specific; validate on your own crop first |
Note that the largest return often comes from the cheapest item on the list. A farm with good aisles and ordinary trolleys will usually beat a farm with automated lines and a congested layout.
Designing for Labour, Not Against It
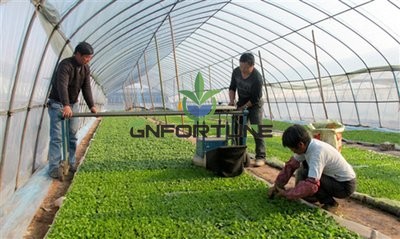
Labour is the largest recurring cost on most hydroponic farms, and layout determines a large share of it. Three questions turn logistics into a labour plan:
- How many metres does a worker walk per shift? Measure it once on an existing site if you can; the number is usually higher and more surprising than expected.
- How many times does a plant change container? Each change is a handling cost and a damage risk. Reducing it is a design decision.
- Where does work concentrate? Harvest, packing and transplanting are peaks. If those three peaks share one aisle, the farm will feel congested at the same hour every day.
Zoning that separates peak operations, even by a few metres, removes most day-to-day congestion without any capital cost.
FAQ
How wide should aisles be on a commercial hydroponic farm?
Wide enough for the largest item that routinely travels there, plus a person, plus a margin. Start from the trolley and crate dimensions you intend to use, then add working clearance — do not start from the space left over after hanging the crop.
Should I use a one-way crop flow?
Yes wherever the building allows it. One-way flow reduces cross-traffic, keeps clean and dirty routes apart, and makes staff behaviour predictable without extra supervision.
Is a harvest conveyor worth it?
It is worth it once volume per bay and the length of the harvest walk are both high. Below that, a well-designed headland and a good trolley usually win on cost.
How do I plan logistics for a vertical farm with narrow aisles?
Accept that access is the constraint and design around it: dedicate specific levels to specific operations, keep a service aisle at the end of every rack, and move people rather than product wherever possible.
Where should the cool room be?
As close to the harvest point as the building permits, on the produce route rather than off a main traffic spine. Every metre between harvest and cooling is paid for in shelf life.
How much does layout change cost after construction?
Enough that it is worth a week of drawing before the first channel is hung. Moving a drain, a door or a power drop later usually costs multiples of the design fee.
Draw the Flow Before You Buy the Racks
Send us your building dimensions, crop plan and target throughput and we will return a layout with crop flow, aisle widths, transfer points and a handling equipment list sized to it. Contact the engineering team through the quote form.
Related reading: logistics feeds directly into labour cost — see harvesting and packing line automation and the wider 7-step project plan, and give your supplier the full picture with the 12 engineering inputs.